#Industry News
How a Liquid Cooling Manifold Gets Made, from Material to Final Acceptance
316L to Helium Testing: The Four Links—Material, Machining, Cleanliness and Verification—That Decide Manifold Quality
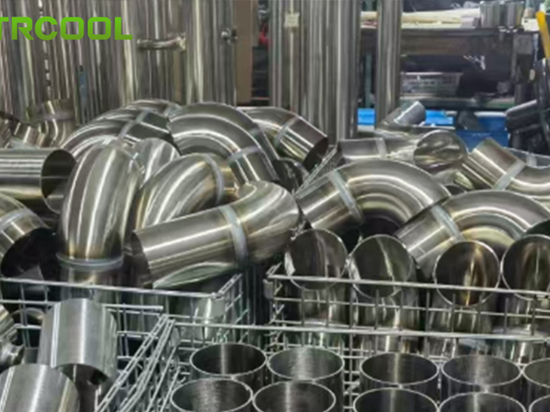
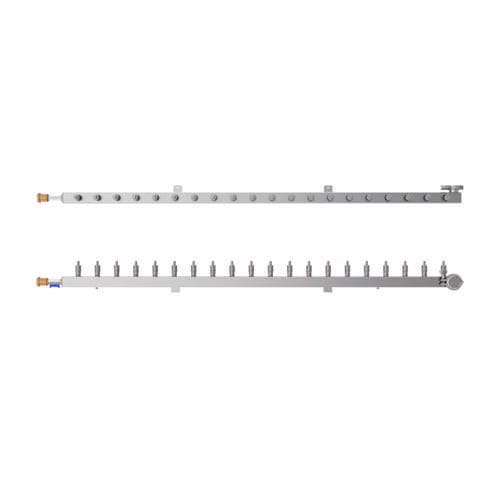
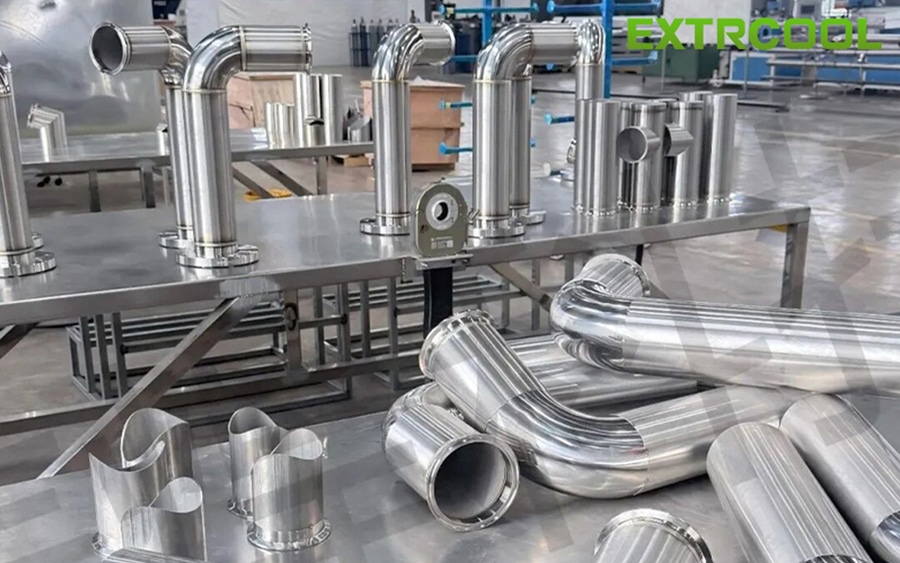
Manifold manufacturing starts with material, and 316L is the safer default, with coolant compatibility outweighing thermal conductivity. CNC machining forms main channels, branches and interface holes, where holding channel positions matters more than drilling; one-piece machining avoids weld deformation, while tube and plate assemblies add laser, TIG or brazing. Deburring, flushing and drying follow, then pressure testing at 100 psi with leak rates below 0.5 mL/min, plus helium mass spectrometry for micro-leaks. Final acceptance prioritizes interface positions, since deviations block connector installation. EXTRCOOL provides one-stop liquid cooling solutions.