
#Industry News
High-Precision Chemical Delivery Module (CDM) for Semiconductor and High-Purity Chemical Distribution
High-Precision Chemical Delivery Module (CDM) for Semiconductor and High-Purity Chemical Distribution
As semiconductor manufacturing continues to move toward smaller process nodes, higher wafer yields, and more advanced fabrication technologies, the precision of chemical delivery systems has become increasingly critical. Modern semiconductor processes such as photolithography, wet cleaning, chemical mechanical polishing (CMP), atomic layer deposition (ALD), and advanced packaging require chemicals to be delivered with exceptional purity, flow stability, and repeatability.
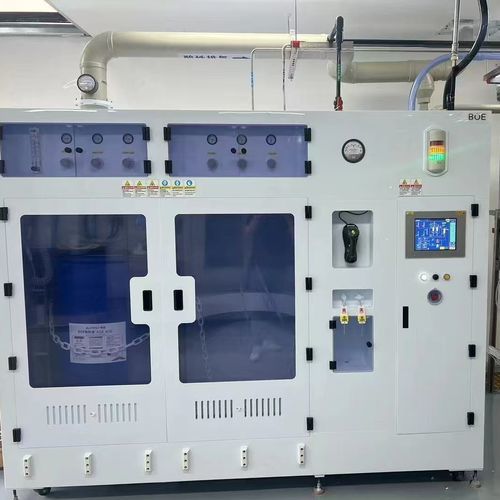
The Chemical Delivery Module (CDM) is the core subsystem responsible for safely transporting ultra-high purity (UHP) chemicals from storage containers to process equipment while maintaining precise control over pressure, flow rate, temperature, and contamination levels.
A high-precision Chemical Delivery Module is far more than a simple pumping system. It integrates advanced fluid engineering, intelligent automation, precision sensors, leak detection, safety interlocks, and contamination control technologies into a highly reliable platform capable of operating continuously in demanding semiconductor cleanrooms.
This article explores the design principles, key components, engineering considerations, safety mechanisms, and future development trends of high-precision Chemical Delivery Modules.
What Is a Chemical Delivery Module (CDM)?
A Chemical Delivery Module (CDM) is an integrated chemical distribution system designed to deliver process chemicals safely and accurately to semiconductor manufacturing equipment.
The module typically handles:
Photoresists
Developers
Solvents
Acids
Bases
DI water
CMP slurries
Specialty chemicals
Cleaning agents
Unlike conventional chemical transfer systems, modern CDMs are engineered to achieve:
Ultra-high purity chemical transport
Accurate flow control
Stable pressure regulation
Zero contamination
Bubble-free delivery
Continuous monitoring
Automatic fault protection
These capabilities directly influence process consistency, wafer quality, and production yield.
Core Design Objectives
Designing a high-performance Chemical Delivery Module involves balancing several engineering objectives simultaneously.
1. Precision Flow Control
One of the primary functions of a CDM is delivering chemicals at a highly stable flow rate.
Typical requirements include:
Continuous flow stability
Minimal flow fluctuation
Fast response to process demand
Repeatable dispensing cycles
Flow precision is achieved through:
Precision diaphragm pumps
Servo-controlled metering pumps
High-resolution flow meters
PID control algorithms
Closed-loop feedback systems
Stable flow prevents coating defects, uneven cleaning, and inconsistent chemical reactions.
2. Ultra-High Purity Design
Semiconductor chemicals are extremely sensitive to contamination.
Even microscopic particles or trace metal ions may result in:
Wafer defects
Particle generation
Device failure
Reduced yield
Therefore, CDMs utilize ultra-clean materials including:
PFA
PTFE
PVDF
High-purity quartz
Electropolished 316L stainless steel
Internal surfaces are designed to minimize:
Particle shedding
Chemical adsorption
Dead volume
Surface roughness
Many systems are assembled and tested inside ISO Class 5 cleanrooms.
Precision Pressure Management
Stable pressure is equally important as stable flow.
Pressure fluctuations may cause:
Chemical splashing
Flow instability
Air entrainment
Process interruption
High-precision CDMs integrate:
Electronic pressure regulators
Pressure transducers
Pneumatic control valves
Automatic relief valves
Closed-loop pressure control continuously adjusts pump speed and valve position according to process demand.
Bubble-Free Chemical Delivery
Air bubbles are among the largest causes of dispensing defects.
Bubble formation can lead to:
Uneven coating
Flow interruption
Inaccurate dosing
Process instability
To eliminate bubbles, CDMs employ:
Degassing Systems
Vacuum degassers remove dissolved gases before chemical delivery.
Bubble Sensors
Ultrasonic bubble detectors identify gas pockets before chemicals enter production equipment.
Optimized Piping
Smooth internal tubing minimizes turbulence and reduces bubble generation.
Intelligent Chemical Level Management
Modern CDMs continuously monitor chemical inventory using multiple sensing technologies.
Common level detection methods include:
Ultrasonic sensors
Load cells
Float switches
Capacitive sensors
The control system automatically performs:
Low-level alarms
Chemical refill requests
Automatic tank switching
Batch tracking
This ensures uninterrupted production.
Accurate Temperature Control
Many semiconductor chemicals exhibit viscosity changes as temperature varies.
Temperature instability may influence:
Pump accuracy
Flow rate
Dispensing precision
Reaction speed
Therefore, high-end CDMs include:
Chemical heaters
Cooling units
Heat exchangers
Temperature sensors
PID temperature controllers
Maintaining a stable chemical temperature significantly improves process consistency.
Advanced Pump Selection
Pump selection determines overall delivery accuracy.
Common pump technologies include:
Diaphragm Pumps
Advantages:
Leak-free operation
High chemical compatibility
Low maintenance
Excellent safety
Applications:
Corrosive chemicals
Acids
Solvents
Magnetically Coupled Pumps
Advantages:
No shaft seal
Zero leakage
Long service life
Applications:
Toxic chemicals
High-purity chemicals
Precision Metering Pumps
Advantages:
Extremely accurate dosing
Programmable dispensing
Repeatable cycles
Applications:
Photolithography
CMP
Chemical blending
Intelligent Automation Architecture
Today’s Chemical Delivery Modules are fully automated systems.
Typical automation components include:
PLC controllers
Industrial PCs
Human Machine Interface (HMI)
SCADA integration
Remote monitoring
Recipe management
Automation enables:
Automatic startup
Chemical switching
Self-diagnostics
Alarm management
Preventive maintenance
Real-time monitoring greatly reduces operator intervention.
Chemical Compatibility Engineering
A single semiconductor fab may use hundreds of chemicals.
These include:
Sulfuric acid
Hydrofluoric acid
Nitric acid
Ammonium hydroxide
Hydrogen peroxide
Isopropyl alcohol
Acetone
NMP
Photoresists
Every wetted component must be carefully selected for compatibility.
Design engineers evaluate:
Corrosion resistance
Chemical permeation
Material swelling
Mechanical strength
Long-term reliability
Material selection directly impacts system lifespan.
Leak Detection and Safety Protection
Chemical safety is one of the highest priorities in CDM design.
Modern systems integrate multiple protection layers.
Leak Sensors
Installed beneath:
Pumps
Valves
Chemical tanks
Cabinets
Leak sensors immediately trigger alarms and emergency shutdown.
Emergency Shutoff Valves
Automatic isolation valves quickly stop chemical flow during abnormal conditions.
Exhaust Ventilation
Chemical cabinets maintain negative pressure ventilation to remove hazardous vapors.
Gas Detection
Some chemicals release toxic or corrosive gases.
Integrated gas detectors monitor:
HF
HCl
NH₃
VOCs
The system automatically activates alarms and exhaust systems when dangerous concentrations are detected.
Redundancy for Continuous Production
Semiconductor fabs operate 24 hours a day.
Unexpected downtime is extremely expensive.
High-end CDMs therefore incorporate redundant designs, including:
Dual pumps
Dual filters
Dual pressure sensors
Dual flow meters
Automatic switchover valves
If one component fails, the backup immediately assumes operation without interrupting production.
Filtration System Design
Particle removal is another essential function.
Typical filtration stages include:
Primary Filter
Removes large particles introduced during chemical transfer.
Fine Filter
Captures submicron contaminants.
Final Ultra-Clean Filter
Installed immediately before the process tool.
Some advanced systems use filtration below 0.05 μm.
This significantly reduces wafer contamination.
Data Acquisition and Industry 4.0 Integration
Modern semiconductor factories rely heavily on digital manufacturing.
A high-precision CDM continuously records:
Flow rate
Pressure
Temperature
Chemical consumption
Alarm history
Pump status
Valve positions
Communication protocols include:
SECS/GEM
OPC UA
Modbus TCP/IP
Ethernet/IP
Profinet
These interfaces enable seamless integration with factory automation systems, Manufacturing Execution Systems (MES), and predictive maintenance platforms.
Energy Efficiency Considerations
Energy consumption has become an important design objective.
Modern CDMs improve efficiency through:
Variable-frequency pump control
Intelligent standby modes
Optimized chemical circulation
Low-power sensors
Smart ventilation management
Reduced energy consumption lowers operational costs while supporting sustainable manufacturing.
Future Development Trends
Chemical Delivery Modules continue evolving alongside semiconductor technology.
Future innovations include:
AI-Based Process Optimization
Artificial intelligence will optimize chemical flow in real time based on production data.
Predictive Maintenance
Machine learning algorithms will detect abnormal operating conditions before failures occur.
Digital Twin Technology
Virtual models will simulate equipment performance, allowing engineers to optimize maintenance schedules and process parameters.
Fully Autonomous Chemical Management
Future CDMs will automatically:
Schedule chemical replenishment
Optimize consumption
Balance production loads
Detect contamination
Generate maintenance reports
Minimal human intervention will further improve safety and production efficiency.
Conclusion
The high-precision Chemical Delivery Module (CDM) has become an indispensable subsystem in semiconductor manufacturing, pharmaceutical production, flat panel display fabrication, and other high-purity industrial applications. Its design extends well beyond simple chemical transfer, integrating advanced fluid dynamics, precision flow and pressure control, ultra-clean materials, intelligent automation, comprehensive safety protection, and real-time data management into a unified platform.
By combining contamination-free fluid paths, closed-loop process control, redundant system architecture, intelligent monitoring, and Industry 4.0 connectivity, modern CDMs deliver the reliability and precision required for today’s most demanding manufacturing environments. As semiconductor technology advances toward increasingly complex process nodes, next-generation Chemical Delivery Modules will leverage AI-driven optimization, predictive maintenance, digital twin technology, and autonomous chemical management to achieve even higher levels of performance, safety, and operational efficiency. For equipment manufacturers and semiconductor fabs seeking maximum yield, stable production, and long-term reliability, investing in a well-engineered, high-precision Chemical Delivery Module is a strategic necessity rather than merely an equipment upgrade.
For more about fully automatic specialty gas cabinet with PLC control, you can pay a visit to Jewellok at https://www.jewellok.com/product-category/chemical-delivery-system/ for more info.