#Industry News
Automated Floor-Level Package Conveying in the Food Industry
Discover an automated floor-level conveyor system designed by OCA to streamline the transport and storage of packages in the food industry.
Optimizing Material Handling Workflows with an Automated Conveyor Solution
In the food processing industry, optimizing logistics workflows is a key factor in improving productivity, reducing the physical strain of workstations, and ensuring the safety of material handling operations. We recently partnered with a poultry producer to fully automate its floor conveyor system and package storage.
Strenuous Manual Handling
Before our conveyor system was installed, operators performed all the handling tasks required for meat production manually.
After weighing and labeling, each package was lifted and placed on a pallet. Once the pallet was full, it was moved to a storage area in an adjacent room.
This setup had several limitations:
- significant physical strain on operators;
- a high risk of musculoskeletal disorders (MSDs);
- a production rate limited by time lost due to the manual handling of meat packages.
A floor conveyor solution tailored to the demands of the food processing industry
To address these challenges, OCA designed and installed fully automated floor conveyors to streamline the transport of packages throughout the production process.
Two modular mesh conveyors were installed along the workstations to serve all operators.
With this configuration, packages of various sizes (cartons and bins) are simply placed on the conveyors, virtually eliminating all manual operations. Operators need only push the packages onto the conveyor, with no manual handling required.
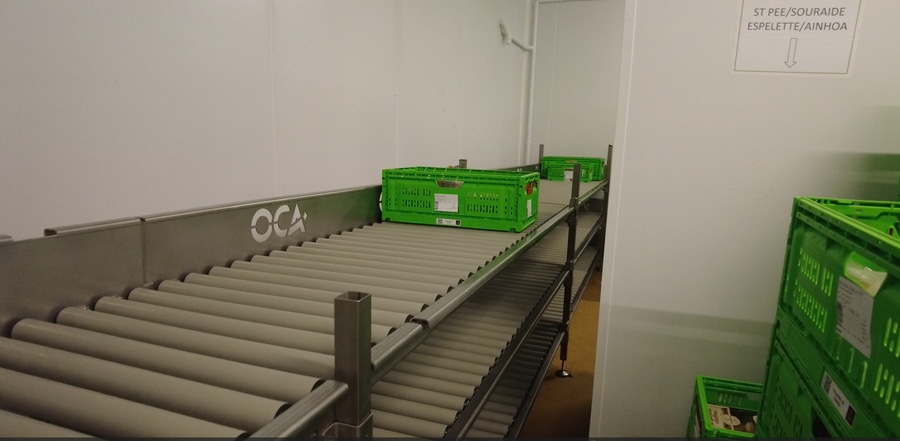
Up to 100 packages per hour are then automatically transported to a gravity storage area via a roller conveyor.
Automated and Intelligent Storage
The system incorporates a swivel conveyor that automatically feeds three levels of gravity storage.
Overflow detection sensors control the distribution of packages across the different levels to ensure:
- a continuous feed to the storage area,
- even distribution of packages,
- uninterrupted operation, even during production peaks.
This automation ensures optimized production flow and storage capacity.
The benefits of this industrial conveyor system
Implementing this solution provides immediate human, organizational, and economic benefits for our client.
- Improved workplace ergonomics: Eliminating lifting tasks significantly reduces the physical strain on operators and helps prevent musculoskeletal disorders (MSDs).
- Increased productivity: Automating material flows speeds up package processing, eliminates unnecessary handling time, and increases production rates.
- Storage optimization: Automated management of different storage levels improves the availability of storage areas while ensuring a continuous supply to the production lines.
- Process reliability: Thanks to automated conveyors, motorized transfers, and detection sensors, the system operates autonomously with a high degree of consistency.
Are you looking to automate your material handling processes?
As a specialist in industrial conveying solutions, OCA designs and builds custom systems to help food and beverage companies automate their production lines, optimize logistics flows, and improve workplace ergonomics.
Each project is tailored to your production constraints, production rates, product characteristics, and performance goals to provide a reliable, scalable conveying solution that integrates seamlessly into your industrial environment.
Contact us